Validate automation before it reaches the plant floor.
We test PLC logic, safety interlocks and industrial networks in high-fidelity digital twins, and harden control systems against the attacks now targeting US infrastructure, so failures and intrusions surface in simulation, not in production.
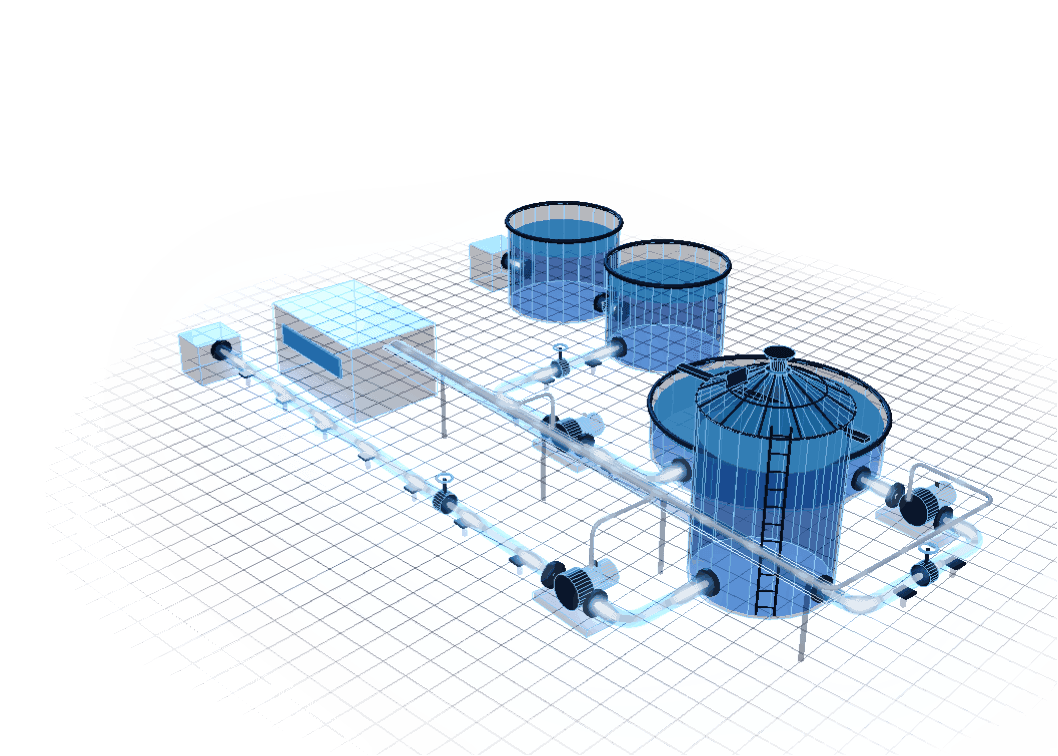
 3D · Digital twin · water treatment plant
Automation Risk Mapping & Operational Resilience
The ARMOR method: five layers that make functional safety and simulation part of the architecture, not an afterthought.
Hazard & risk mapping
Classify safety-critical processes against OSHA PSM, Machine Guarding and FDA 21 CFR 117.
Functional safety design
Architectures built to IEC 61508 and ISA 84 / IEC 61511 to prevent, detect and mitigate failures.
Virtual validation
Digital twins stress-test logic, interlocks and networks before commissioning.
Audit readiness
Controls that flag unauthorized changes and integrity deviations, aligned with 21 CFR Part 11.
Risk monitoring
Ongoing review of performance and risk indicators as systems evolve, including the AI that helps build them.
Your PLCs are a target. We know how they’re attacked.
Federal alerts warn of coordinated attacks on internet-exposed PLCs in US water systems: passwords changed, operators locked out, processes disrupted. Our engineers hold OT cybersecurity certifications and train continuously, keeping pace with evolving industrial security standards and the latest threat advisories.
What attackers look for
- PLCs and HMIs exposed to the public internet
- Default or shared passwords
- Flat networks between IT and OT
- Undocumented remote access, like cellular modems
Exposure assessment
Find every PLC, HMI and remote path reachable from outside before an attacker does.
Hardening & segmentation
Credentials, firmware, allow-lists and network zones built to IEC 62443 practice.
Attack simulation
We replay real attack paths against the digital twin to prove the plant fails safe.
Specialists where failure is not an option
Pharmaceutical
Validated processes where every recipe change, alarm and audit trail has to hold up to an FDA inspection. We test control logic in a digital twin before it touches a GMP batch.
- Audit trails and electronic records per 21 CFR Part 11
- Batch logic and interlocks validated before release
- Change control backed by simulation evidence
- Part 11
- audit trails and electronic records
- Digital twin
- batch logic tested before go-live
- IEC 62443
- OT security practice
- ISA 84
- safety instrumented functions
Food & beverage
High-speed lines where a guarding fault or a wrong recipe parameter means an injury or a recall. We validate machine safety and process logic before production restarts.
- Machine guarding aligned with OSHA 1910.212
- Preventive controls supported per FDA 21 CFR Part 117
- Line changeovers simulated before they hit the floor
- 1910.212
- machine guarding
- Part 117
- preventive controls
- Digital twin
- changeovers tested offline
- IEC 62443
- OT security practice
Chemical & industrial furnaces
Reactors, furnaces and hazardous processes where a failed interlock can become a release. We engineer and test safety functions before the first startup.
- Process safety aligned with OSHA PSM 1910.119
- Burner management and furnace interlocks validated in simulation
- SIS lifecycle per ISA 84 / IEC 61511
- 1910.119
- process safety management
- ISA 84
- IEC 61511 safety lifecycle
- IEC 61508
- functional safety
- IEC 62443
- OT security practice
Water & wastewater
Treatment and distribution systems where one compromised PLC can stop safe drinking water. We secure and validate the control layer end to end.
- Internet exposure removed from PLCs and SCADA
- Setpoint and logic changes validated before they go live
- Remote sites and telemetry secured
- SCADA
- telemetry and remote sites secured
- 0
- PLCs left exposed online
- IEC 62443
- OT security practice
- ISA 84
- safety instrumented functions
Two thousand degrees of process. Zero guesswork in control.
Scroll to open the furnace and see where RHJ automation does its work.Swipe through the furnace and see where RHJ automation does its work.
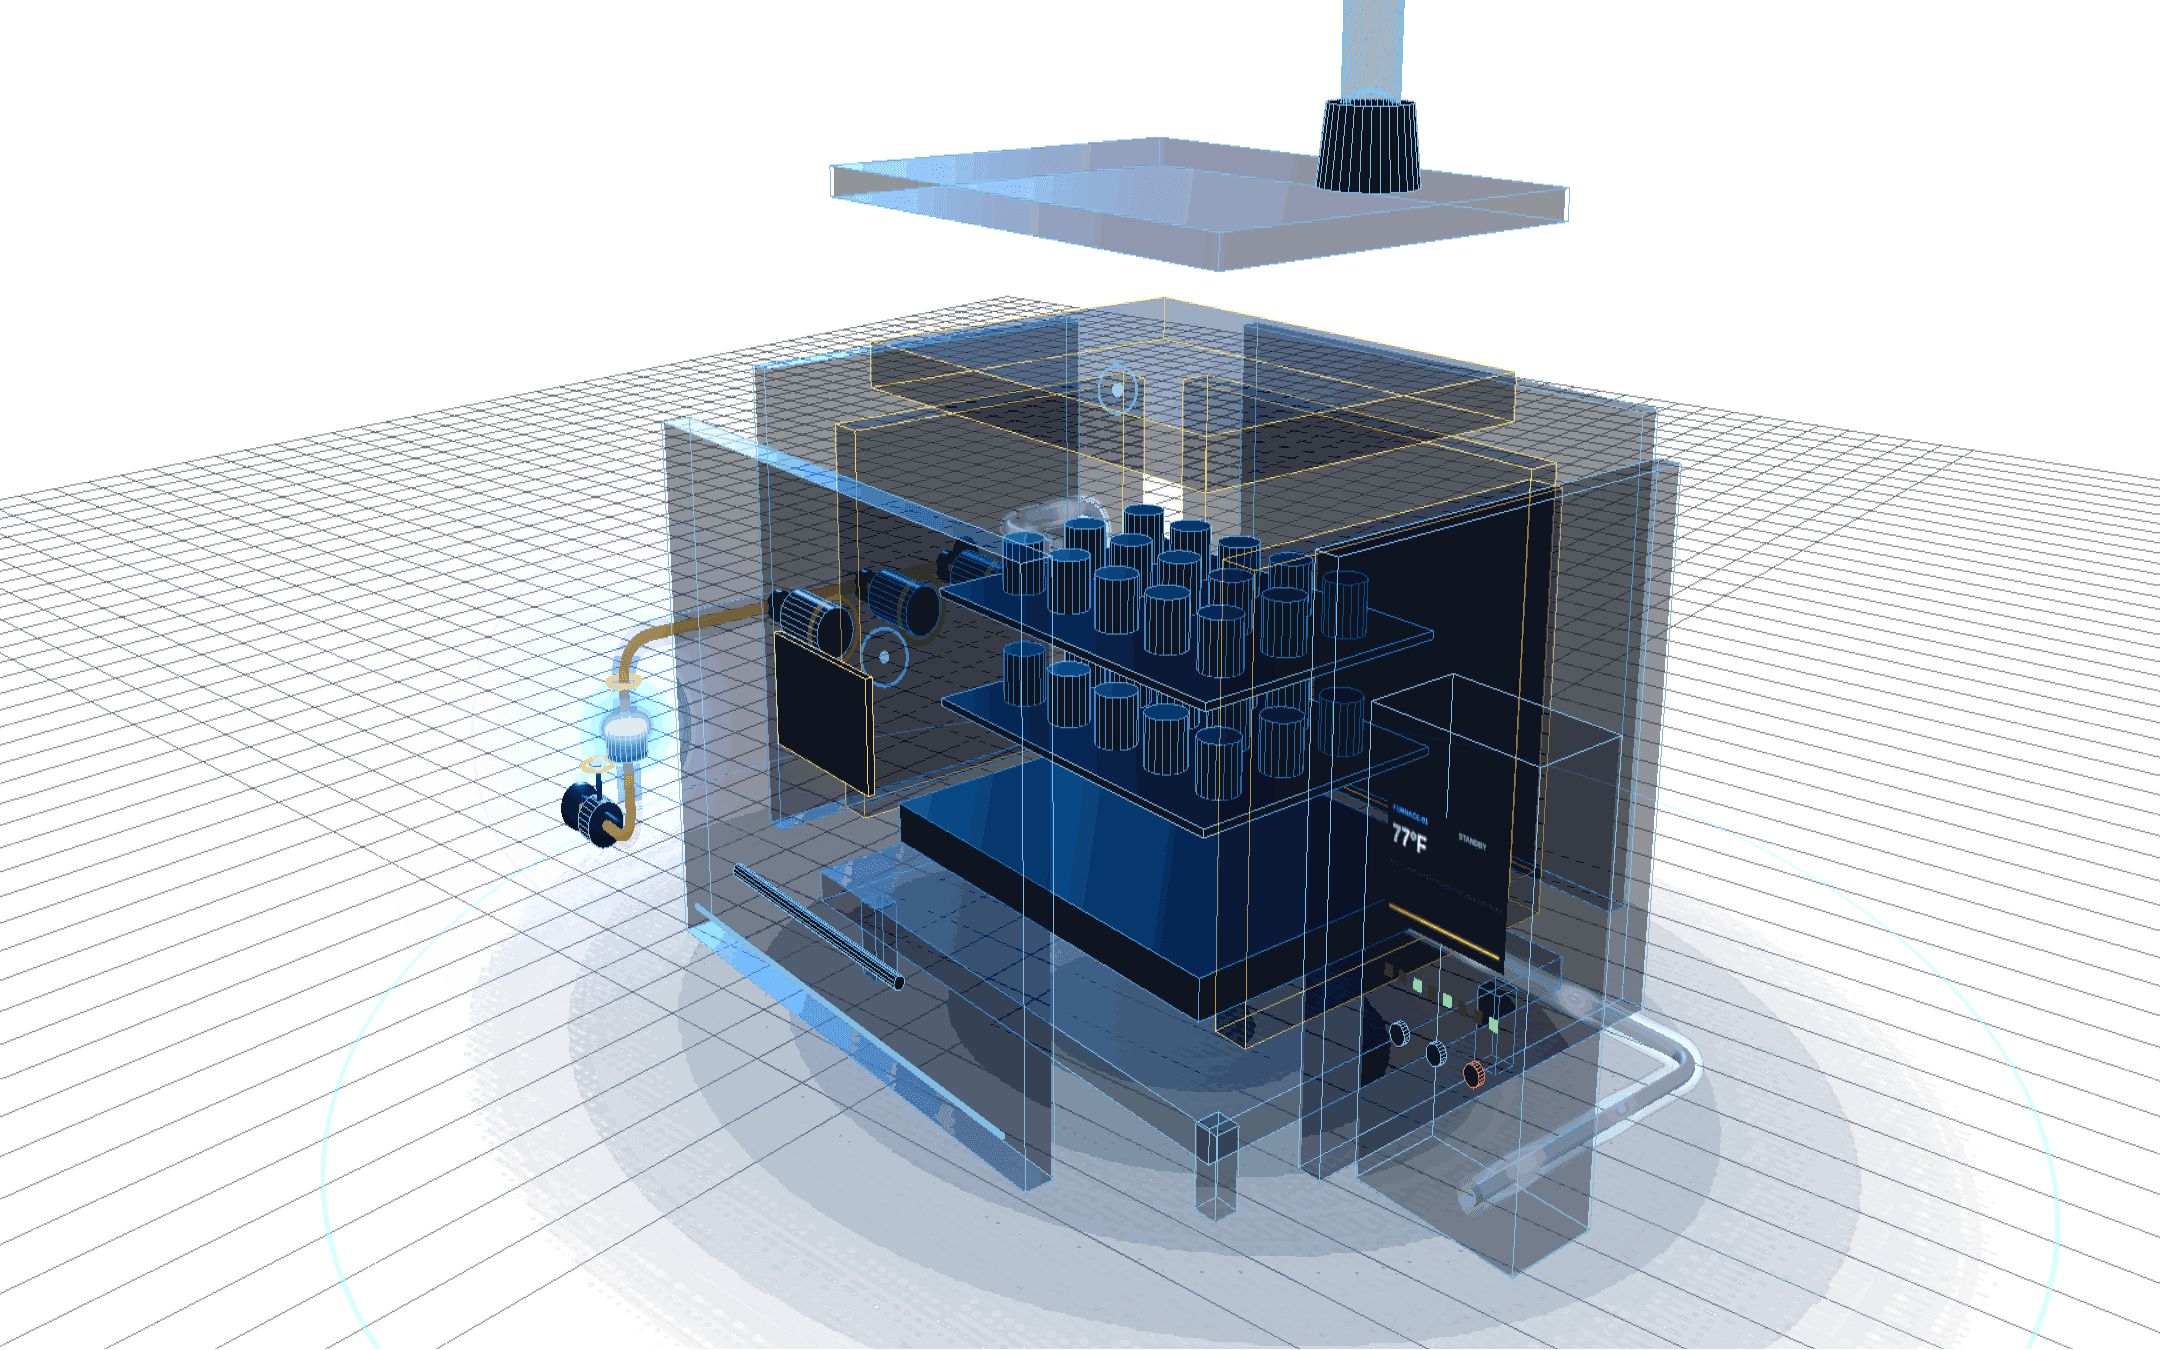
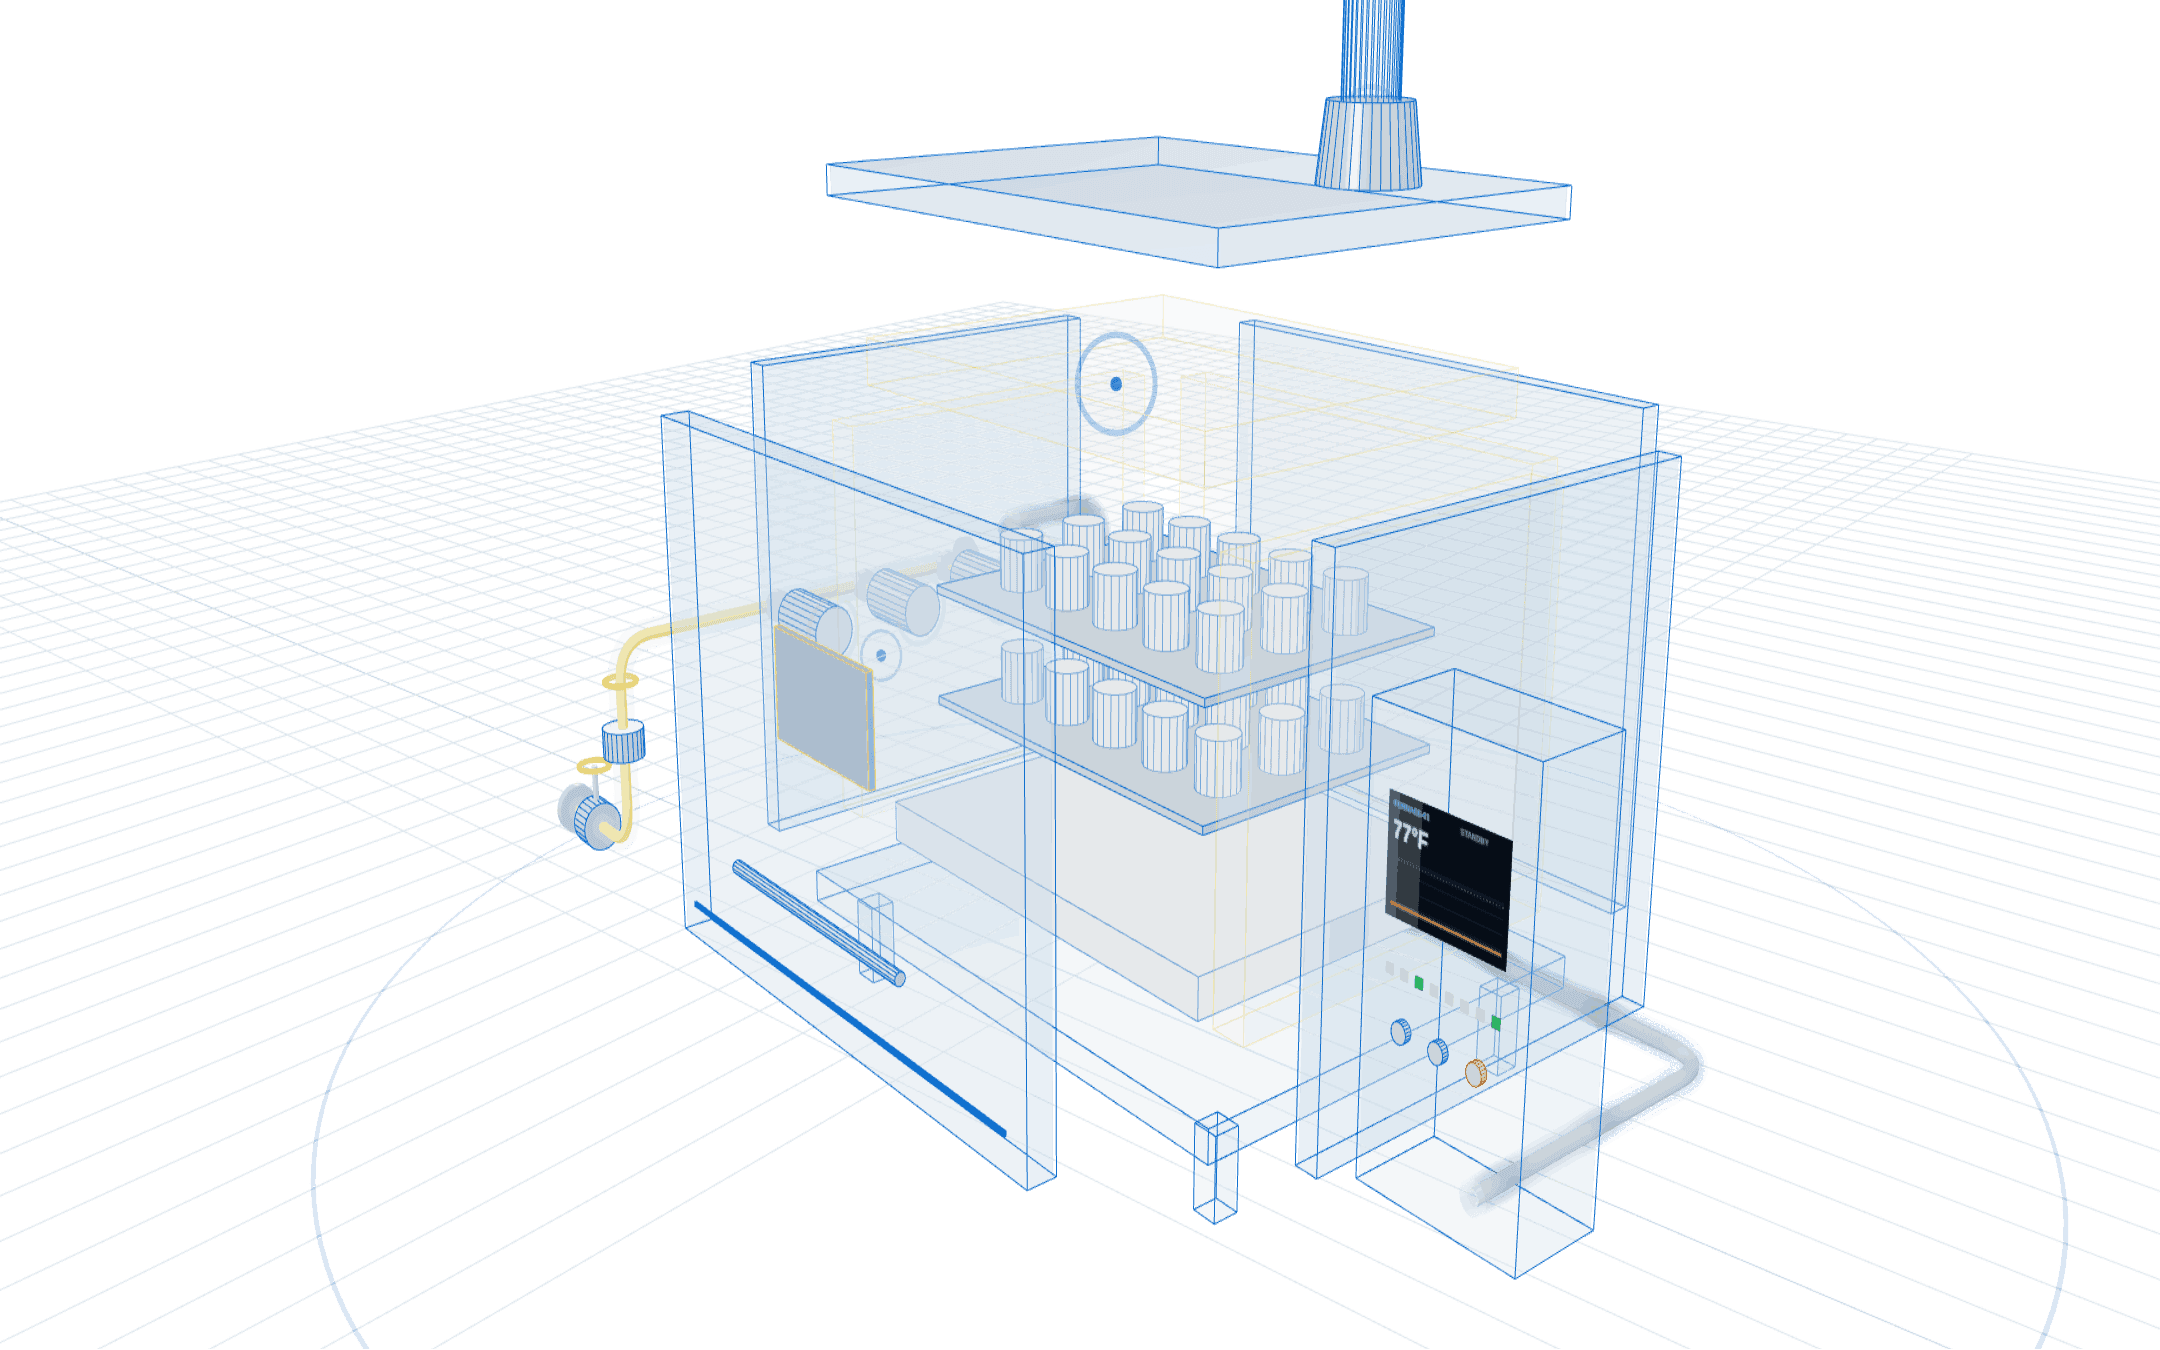
Chamber furnace
Steel casing, front door with sight glass and top exhaust flue.
Layer by layer
Refractory lining, load chamber and side-mounted burners.
Validated before startup
Burner logic and flame safety interlocks tested in a digital twin before the first ignition.
Controlled ignition
Burners firing, temperature ramping, every value visible on SCADA.
Validated by design. Ready for FDA inspection.
In regulated plants, every control-system change is a compliance event. We build and validate the controls behind your electronic records and preventive controls, and keep the evidence audit-ready.
Every change signed and traceable
- 08:14:02Setpoint TIC-101 · 72.0 → 74.0 °FEng-02 · 08:14:02signed
- 08:14:40Change CR-2291 reviewed and approvedQA-Lead · 08:14:40signed
- 08:21:15Batch 24-118 startedOperator-07 · 08:21:15signed
- 08:22:03Unauthorized write blocked · PLC-3System · 08:22:03flagged
- 08:30:00Record locked · checksum verifiedSystem · 08:30:00locked
Electronic records & signatures
Audit trails, access control and e-signatures on SCADA, HMI and batch systems, with real-time detection of unauthorized changes.
Preventive controls, automated
Process controls and monitoring that support FDA food CGMP and preventive controls, with records your quality team can trust.
Safety commissioning built on federal mandates and international standards
We connect what federal rules require with how technical standards say to do it: OSHA and FDA mandates, engineered and evidenced to ISA 84 / IEC 61511 and IEC 61508.
OSHA PSM + Machine Guarding × ISA 84 / IEC 61511 in one framework. Verifiable. Audit-ready.
- SIL
- determination and verification
- LOPA
- layer of protection analysis
- FTA
- fault tree analysis
- Audit-ready
- technical files for FDA and OSHA inspections
OSHA Process Safety Management
Federal requirements for managing highly hazardous chemical processes.
OSHA Machine Guarding
Safeguarding requirements for machinery and moving parts.
Functional Safety
Safety of electrical, electronic and programmable safety-related systems.
Safety Instrumented Systems
Functional safety lifecycle for the process industry.
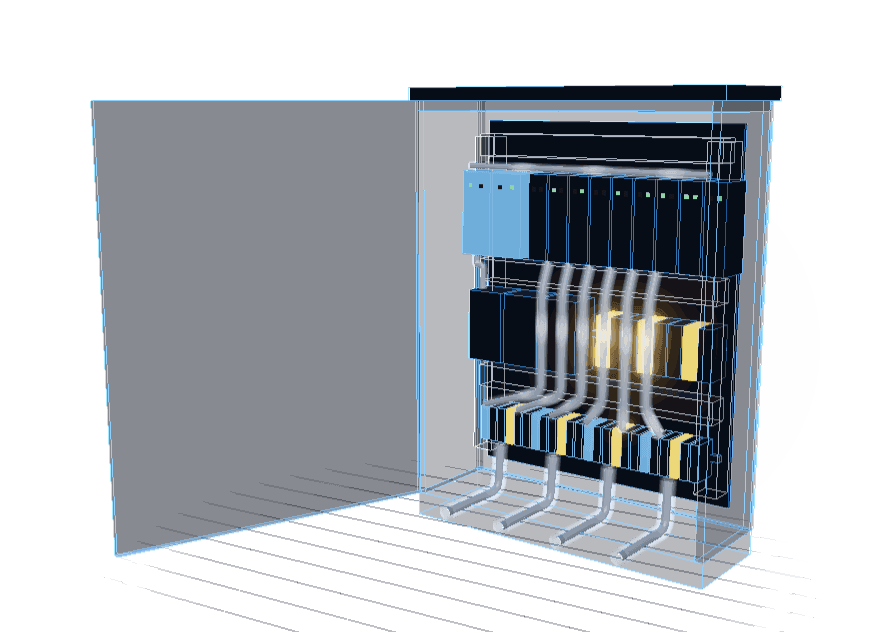
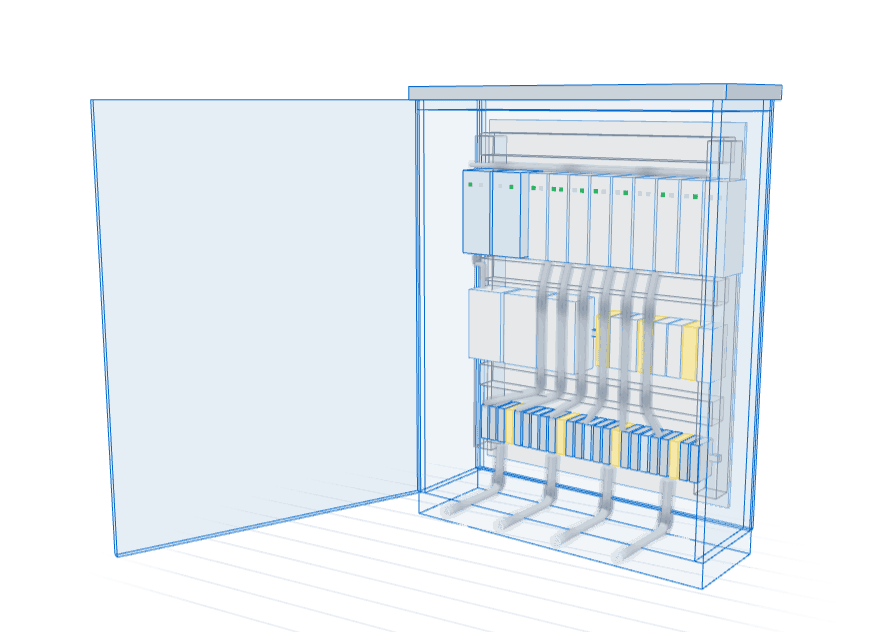
Panels and logic designed to fail safe
- Redundant CPU
- Automatic failover with no process interruption.
- Distributed I/O
- Input and output modules installed close to the field.
- Interlocks
- Logic that blocks unsafe operating conditions.
- Diagnostics
- Status of every module visible on SCADA.
Systemic Technical Expertise & Engineering Readiness
The STEER method. ARMOR secures the system, STEER readies the people who run it: a standard protocol that embeds engineering expertise in your team, so everything we deploy is operated, sustained and audited in-house.
Integrated competency
Senior engineering expertise transferred to your automation team, architecting fail-safe systems to OSHA standards.
Applied failure scenarios
Real regulatory cases and automation failure modes prepare technicians for high-stakes decisions.
Virtual systems immersion
Operators rehearse on the digital twin, a zero-risk simulator, before the plant goes live.
Operational reliability
The OSHA and FDA requirements that apply to each task, built into your standard operating procedures.
Peer-to-peer mentorship
Knowledge transfer embedded in every deployment, not sold as a separate service.
- 01CommissioningStartup and testing with the live process.
- 02TrainingHands-on training for operators and maintenance staff.
- 03Assisted operationOn-site support through the first weeks.
- 04ComplianceDocumentation for regulatory requirements and audits.
What clients and students say
“RHJ’s safety commissioning team closed, in just two weeks, a compliance gap that had been open for months.”
“The courses are straight to the point. I was applying it on the plant floor the same week.”
“Extremely well-prepared technical team, with excellent teaching for beginners.”
Find the failure in simulation, not in production.
Talk to an engineer about validating your next commissioning, upgrade or AI-assisted code change.